

BB Tool
HSS-PM Hexagon Rotary Broach | Internal Hex Broaching Tool for CNC Lathes
HSS-PM Hexagon Rotary Broach | Internal Hex Broaching Tool for CNC Lathes
No se pudo cargar la disponibilidad de retiro
HSS-PM Hexagon Rotary Broach
Internal hex rotary broach for producing hexagonal profiles on lathes, CNC lathes and compatible machining setups. Select the hex size and shank/holder format required by your broaching system.
Selection Checklist
- Required internal hex size
- Broach shank size / holder compatibility
- Through-hole or blind-hole application
- Prepared pilot-hole diameter and depth
- Workpiece material and machine rigidity
Important Setup Note
Rotary broaching requires a compatible holder and a correctly prepared pilot hole. The broach itself and holder should be selected as a matched system.


HSS-PM Tool Material
Improving the overall wear resistance and toughness of cutting tools to extend their service life

Internal Hex Rotary Broaching
Rotary broaching can produce internal polygonal profiles such as hexagons and other compatible shapes in prepared blind or through holes.

Machining Reference
Feed 0.03-0.06mm per revolution, copper aluminum processing 2-3 times efficient and fast, with one hole per second

Recommended Processing Equipment
Suitable for general lathes, CNC automatic lathes, comprehensive processing machines, drilling machines and machines with special functions. It is also suitable for punching various standard or special internal and external holes.


Case Presentation
Installed On The Machining Center
Example: Machining spline m=1z=16 deep 20mm
1. Speed: S=1000r/min
2. Feed: F=20m
3. Processing time: 3 minutes (divided into multiple cuts)
Installed on the Lathe
Example: Processing hexagonal 10 with a depth of 15mm on opposite sides
1. Speed: S=1000/min
2. Feed: F=40mm/min
3. Processing time: 20s

Note:
The rotary broach holder is not included unless explicitly stated (if needed, please click on the following image to purchase)
Rotary Torx Broach


BB Hexagon Rotary Broach
Rotary broaching can produce internal polygonal profiles such as hexagons and other compatible shapes in prepared blind or through holes.
Suitable for general lathes, CNC automatic lathes, comprehensive processing machines, drilling machines and machines with special functions. It is also suitable for punching various standard or special internal and external holes.
Material
①HSS-Co M35
②HSS-Powder metallurgy high speed steels
③Tungsten Carbide
*Some sizes need to be customized in about a week
1/16''=1.62 , 1/8''=3.26 , 3/8''=9.6

Drill Hole
The normal drilling of the hexagonal hole must be slightly larger than the effective size of the two-phase plane to which the hole is broached.
Hex S=6~10mm, allowable tolerance +0.06~+0.12mm
Generally, we suggest that the depth of drilling is 1.3 to 1.5 times of the depth of broach hole.

Rotating speed
The principle of BB rotary broach allows it to be applied to high rotating speed, from 600 to 2000 r/min minutes, because rotary speed does not affect the cutting speed. However, at very high speed, when the processing starts, the punch will rub with the workpiece until the speed is synchronized. In this way, it is very easy to wear out the punching knife in advance when using the small punching knife frequently. In order to avoid this phenomenon, it takes 500 r/min minutes at the beginning and the feed is 0. 1mm/turn, when the punch enters the working state, increase the rotation speed.
Feed
The selection of feed is based on the characteristics of the material. In medium carbon steel, if the machine has enough thrust, we suggest that the feed rate of each feed is 0.03~0.06mm. In copper and aluminum materials, two or even three times of the feed volume can be used. In the processing of large axle size and hard-to-cut materials, the feed rate must be reduced by 0.01mm.
Through Hole and blind hole
Generally, there is no need to consider the problem of chip removal when passing through the hole, as long as the depth is noted and the punch is long enough to be customized.
After the blind hole is reserved enough depth, the hexagonal hole should be punched. After the hexagonal hole is finished, the inner hole should be drilled with the drill bit of the previous base hole to discharge the residual debris. Note that the drill bit should be at least 0.1mm smaller than the side of the hexagon, and it cannot touch the inner wall of the hexagon when drilling chips.
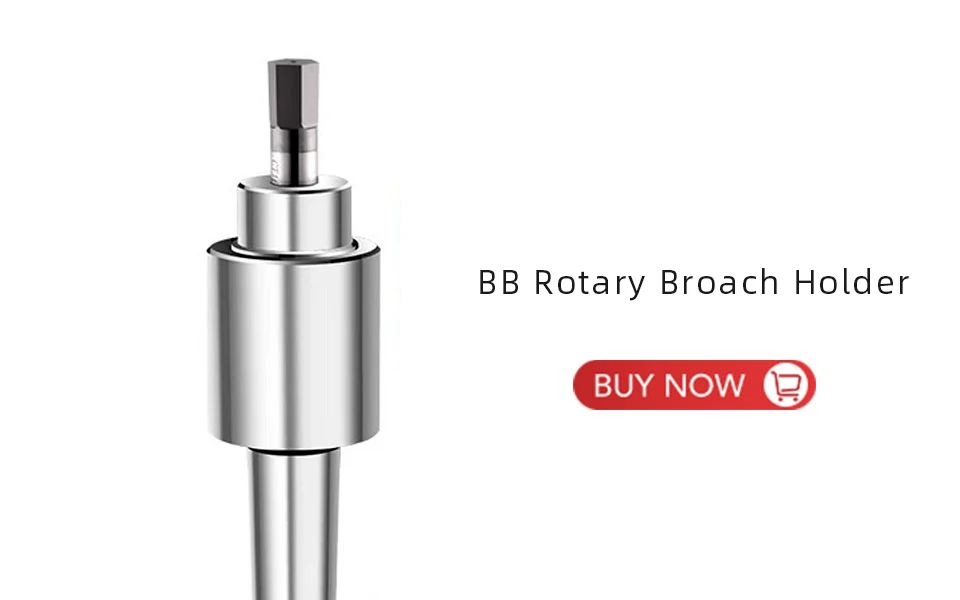
BB Rotary Broach Holder
FAQ
Is the holder included?
Check the selected listing and variant carefully. The broach and holder are separate components unless explicitly stated otherwise.
Can it be used for blind holes?
Blind-hole broaching requires enough pilot-hole depth and chip-clearance planning.


