

BB Tool
HSS-Co Spiral Point Tap | UNC / UNF Inch Threads | TiN
HSS-Co Spiral Point Tap | UNC / UNF Inch Threads | TiN
受取状況を読み込めませんでした
HSS-Co Machine Tap
For machine tapping / CNC use where applicable. Use suitable cutting fluid and select speed according to thread size, workpiece material, tap geometry and machine conditions. The original reference range shown for this product is 500–800 rpm.
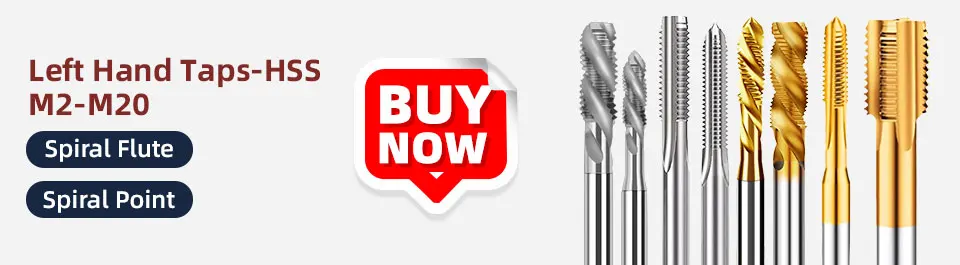
①Straight flute with spiral point.
②Straight flute
③Spiral flute
④Fluteless


HSS-Co Material
HSS-Co provides a practical balance of toughness and wear resistance for tapping stainless steel and other compatible metals.

Ground Thread Geometry
Precision-ground thread geometry and cutting edges support consistent tapping when the correct pilot hole and cutting conditions are used.

Square Drive
Square drive section for secure engagement with a compatible tap holder.

Chip Control
Tap geometry should be selected according to blind-hole or through-hole chip-flow requirements.

TiN & TiCN Selectable
TiN and TiCN coating options are available to improve surface wear resistance and lubricity compared with uncoated versions.

Spiral Flute
Chip direction: upward.
Typical use: blind-hole tapping.
Spiral flutes help evacuate chips away from the bottom of the hole.
Spiral Point
Chip direction: forward/downward.
Typical use: through-hole tapping.
Spiral-point geometry pushes chips ahead of the tap in compatible steels and alloys.


Tapping Speed Reference
Tapping speed depends on workpiece material, pilot-hole condition, tap geometry, coating, cutting fluid and machine capability. Use the reference table below as a starting point and adjust to actual machine and workpiece conditions.


